Commissioning a Gear Hobbing Machine: A Measurement-Led Procedure

Key Takeaways:

A measurement-led commissioning procedure for gear hobbing machines that closes the loop against ISO 1328 gear inspection.

Tags:
gear hobbing machine commissioning gear machine alignment laser axis calibration ISO 1328 gear inspection hobbing test gear measurement

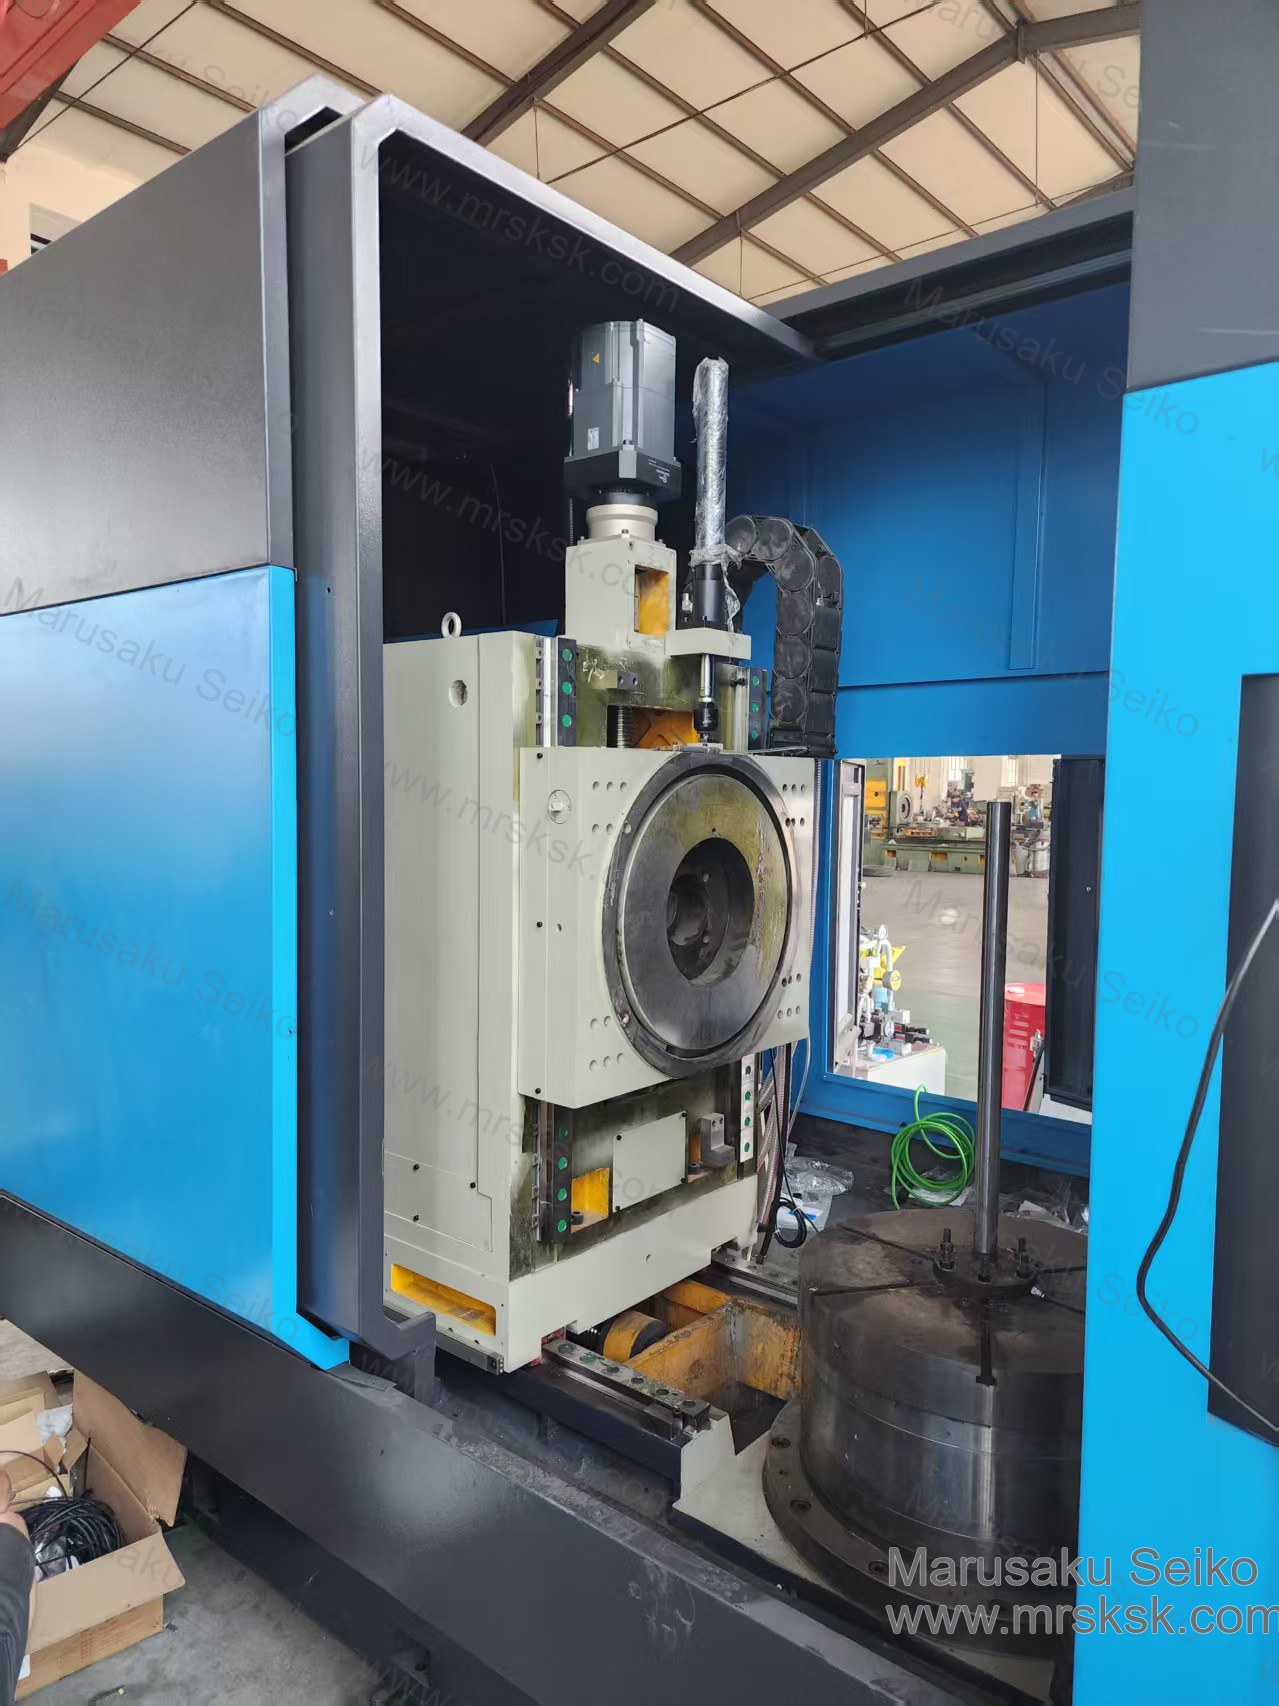
Commissioning a gear hobbing machine is not "install, level, run a part." It is a measurement-led loop: bring the machine into geometric truth, prove it with a test gear inspected to the ISO 1328 system, correct what the measurement shows, and repeat until the grade holds hot. Here is the sequence that separates a machine that ships correct from one that ships hopeful.

1. Foundation and levelling

Set the bed on its supports, level within the builder's tolerance, and let it settle. Thermal and geometric truth both start here; a twisted foundation cannot be calibrated out later.

2. Spindle and axis runout checks

Verify work-table radial and axial runout and hob-spindle radial runout per the machine's geometric acceptance (the ISO 230 family of machine-tool tests governs this step). Record the numbers — they become the baseline the gear measurements are later compared against.

3. Oil conditioning and warm-up

For hydrostatic machines, circulate and condition the oil to its working temperature before any accuracy work. A cold hydrostatic film is a different geometry from a warm one; skipping warm-up is the most common reason a machine "fails commissioning" on the first parts and passes on the fourth.

4. Axis calibration

Calibrate the linear axes with a laser interferometer and verify the rotary (C and B) axes against their encoders. Map and compensate the residuals. This is where squareness and pitch errors — the ones that become helix taper and pitch drift — are caught.

5. Test-cut and measure against ISO 1328

Cut a representative gear in the production material and measure it on an analytical gear checker under the ISO 1328 geometry definition: profile deviation ffα, helix deviation fHβ, cumulative and single-pitch deviations Fp/fpt, and radial runout Fr. A two-flange (double-flank) rolling test is useful for a quick composite read; the analytical check is what the grade is actually written from. Note the deliberate choice here: this is the ISO system, not any national (GB) standard — the grade numbers mean the same thing internationally.

6. Close the loop on the errors you found

  • Helix taper / slope → feed-axis squareness or axial misalignment.
  • Pitch drift across the gear → C-axis indexing or thermal soak.
  • Radial runout → work-table centering or spindle runout.
  • Profile bow → hob runout or B-axis swivel.

Adjust, re-cut, re-measure. Commissioning ends when the grade holds across a warm, fully loaded run — not when the first part looks close.

7. Document and hand over

Keep the runout logs, laser maps, and the final ISO 1328 gear report together. A commissioning file that only says "ran OK" is worthless the day a customer questions a grade. Selecting the right machine for the job in the first place also shortens this loop — our CNC gear hobbing machine selection guide is where that decision starts.
Available Languages
🇬🇧 English

Commissioning a Gear Hobbing Machine: A Measurement-Led Procedure

Commissioning a gear hobbing machine is not "install, level, run a part." It is a measurement-led loop: bring the machine into geometric truth, prove it with a test gear inspected to the ISO 1328 system, correct what the measurement shows, and repeat until the grade holds hot. Here is the sequence that separates a machine that ships correct from one that ships hopeful.

1. Foundation and levelling

Set the bed on its supports, level within the builder's tolerance, and let it settle. Thermal and geometric truth both start here; a twisted foundation cannot be calibrated out later.

2. Spindle and axis runout checks

Verify work-table radial and axial runout and hob-spindle radial runout per the machine's geometric acceptance (the ISO 230 family of machine-tool tests governs this step). Record the numbers — they become the baseline the gear measurements are later compared against.

3. Oil conditioning and warm-up

For hydrostatic machines, circulate and condition the oil to its working temperature before any accuracy work. A cold hydrostatic film is a different geometry from a warm one; skipping warm-up is the most common reason a machine "fails commissioning" on the first parts and passes on the fourth.

4. Axis calibration

Calibrate the linear axes with a laser interferometer and verify the rotary (C and B) axes against their encoders. Map and compensate the residuals. This is where squareness and pitch errors — the ones that become helix taper and pitch drift — are caught.

5. Test-cut and measure against ISO 1328

Cut a representative gear in the production material and measure it on an analytical gear checker under the ISO 1328 geometry definition: profile deviation ffα, helix deviation fHβ, cumulative and single-pitch deviations Fp/fpt, and radial runout Fr. A two-flange (double-flank) rolling test is useful for a quick composite read; the analytical check is what the grade is actually written from. Note the deliberate choice here: this is the ISO system, not any national (GB) standard — the grade numbers mean the same thing internationally.

6. Close the loop on the errors you found

  • Helix taper / slope → feed-axis squareness or axial misalignment.
  • Pitch drift across the gear → C-axis indexing or thermal soak.
  • Radial runout → work-table centering or spindle runout.
  • Profile bow → hob runout or B-axis swivel.

Adjust, re-cut, re-measure. Commissioning ends when the grade holds across a warm, fully loaded run — not when the first part looks close.

7. Document and hand over

Keep the runout logs, laser maps, and the final ISO 1328 gear report together. A commissioning file that only says "ran OK" is worthless the day a customer questions a grade. Selecting the right machine for the job in the first place also shortens this loop — our CNC gear hobbing machine selection guide is where that decision starts.